Efficient storage is one of the most important foundations of a productive warehouse, manufacturing plant, construction site, distribution center, or commercial facility. When goods are long, bulky, irregularly shaped, or difficult to handle with conventional pallets, standard shelving and pallet racking often create unnecessary limitations. Pipes, lumber, steel bars, carpets, rolls of material, metal profiles, timber panels, and other oversized products require a storage system that provides strength, accessibility, flexibility, and safe handling.
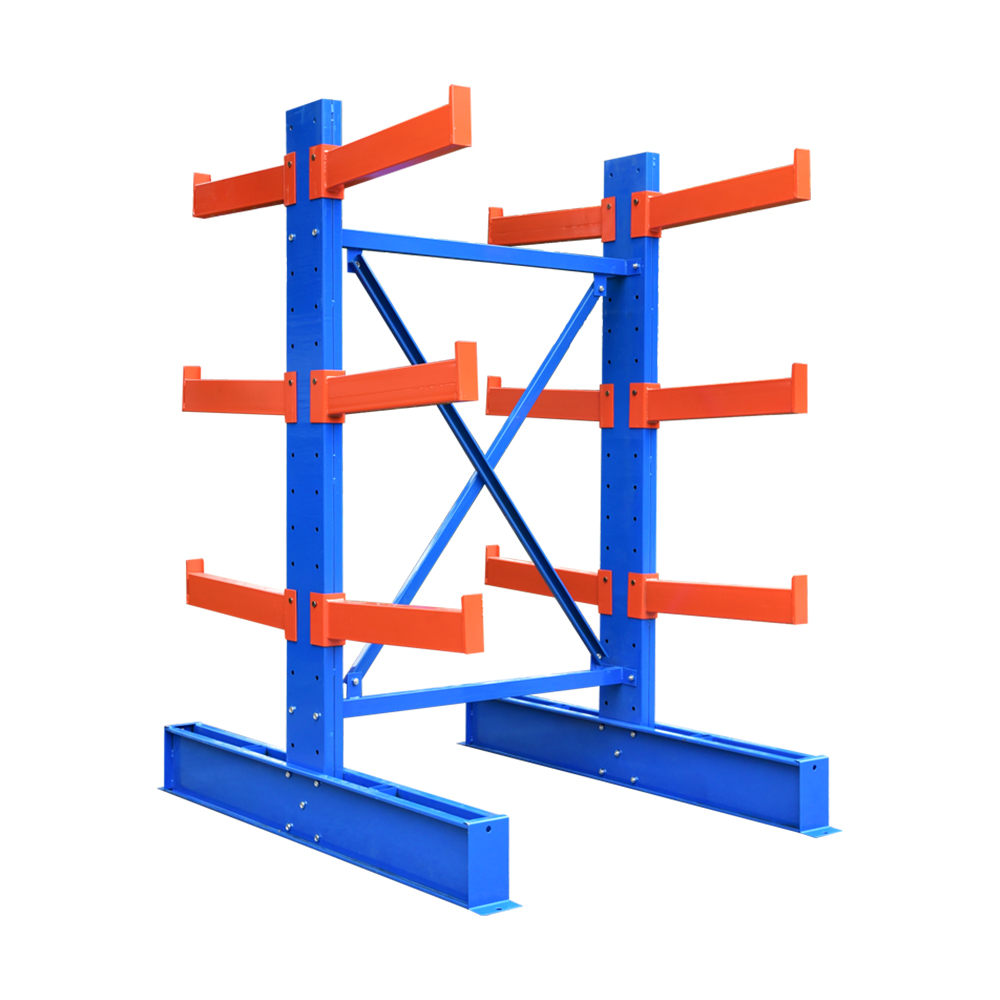
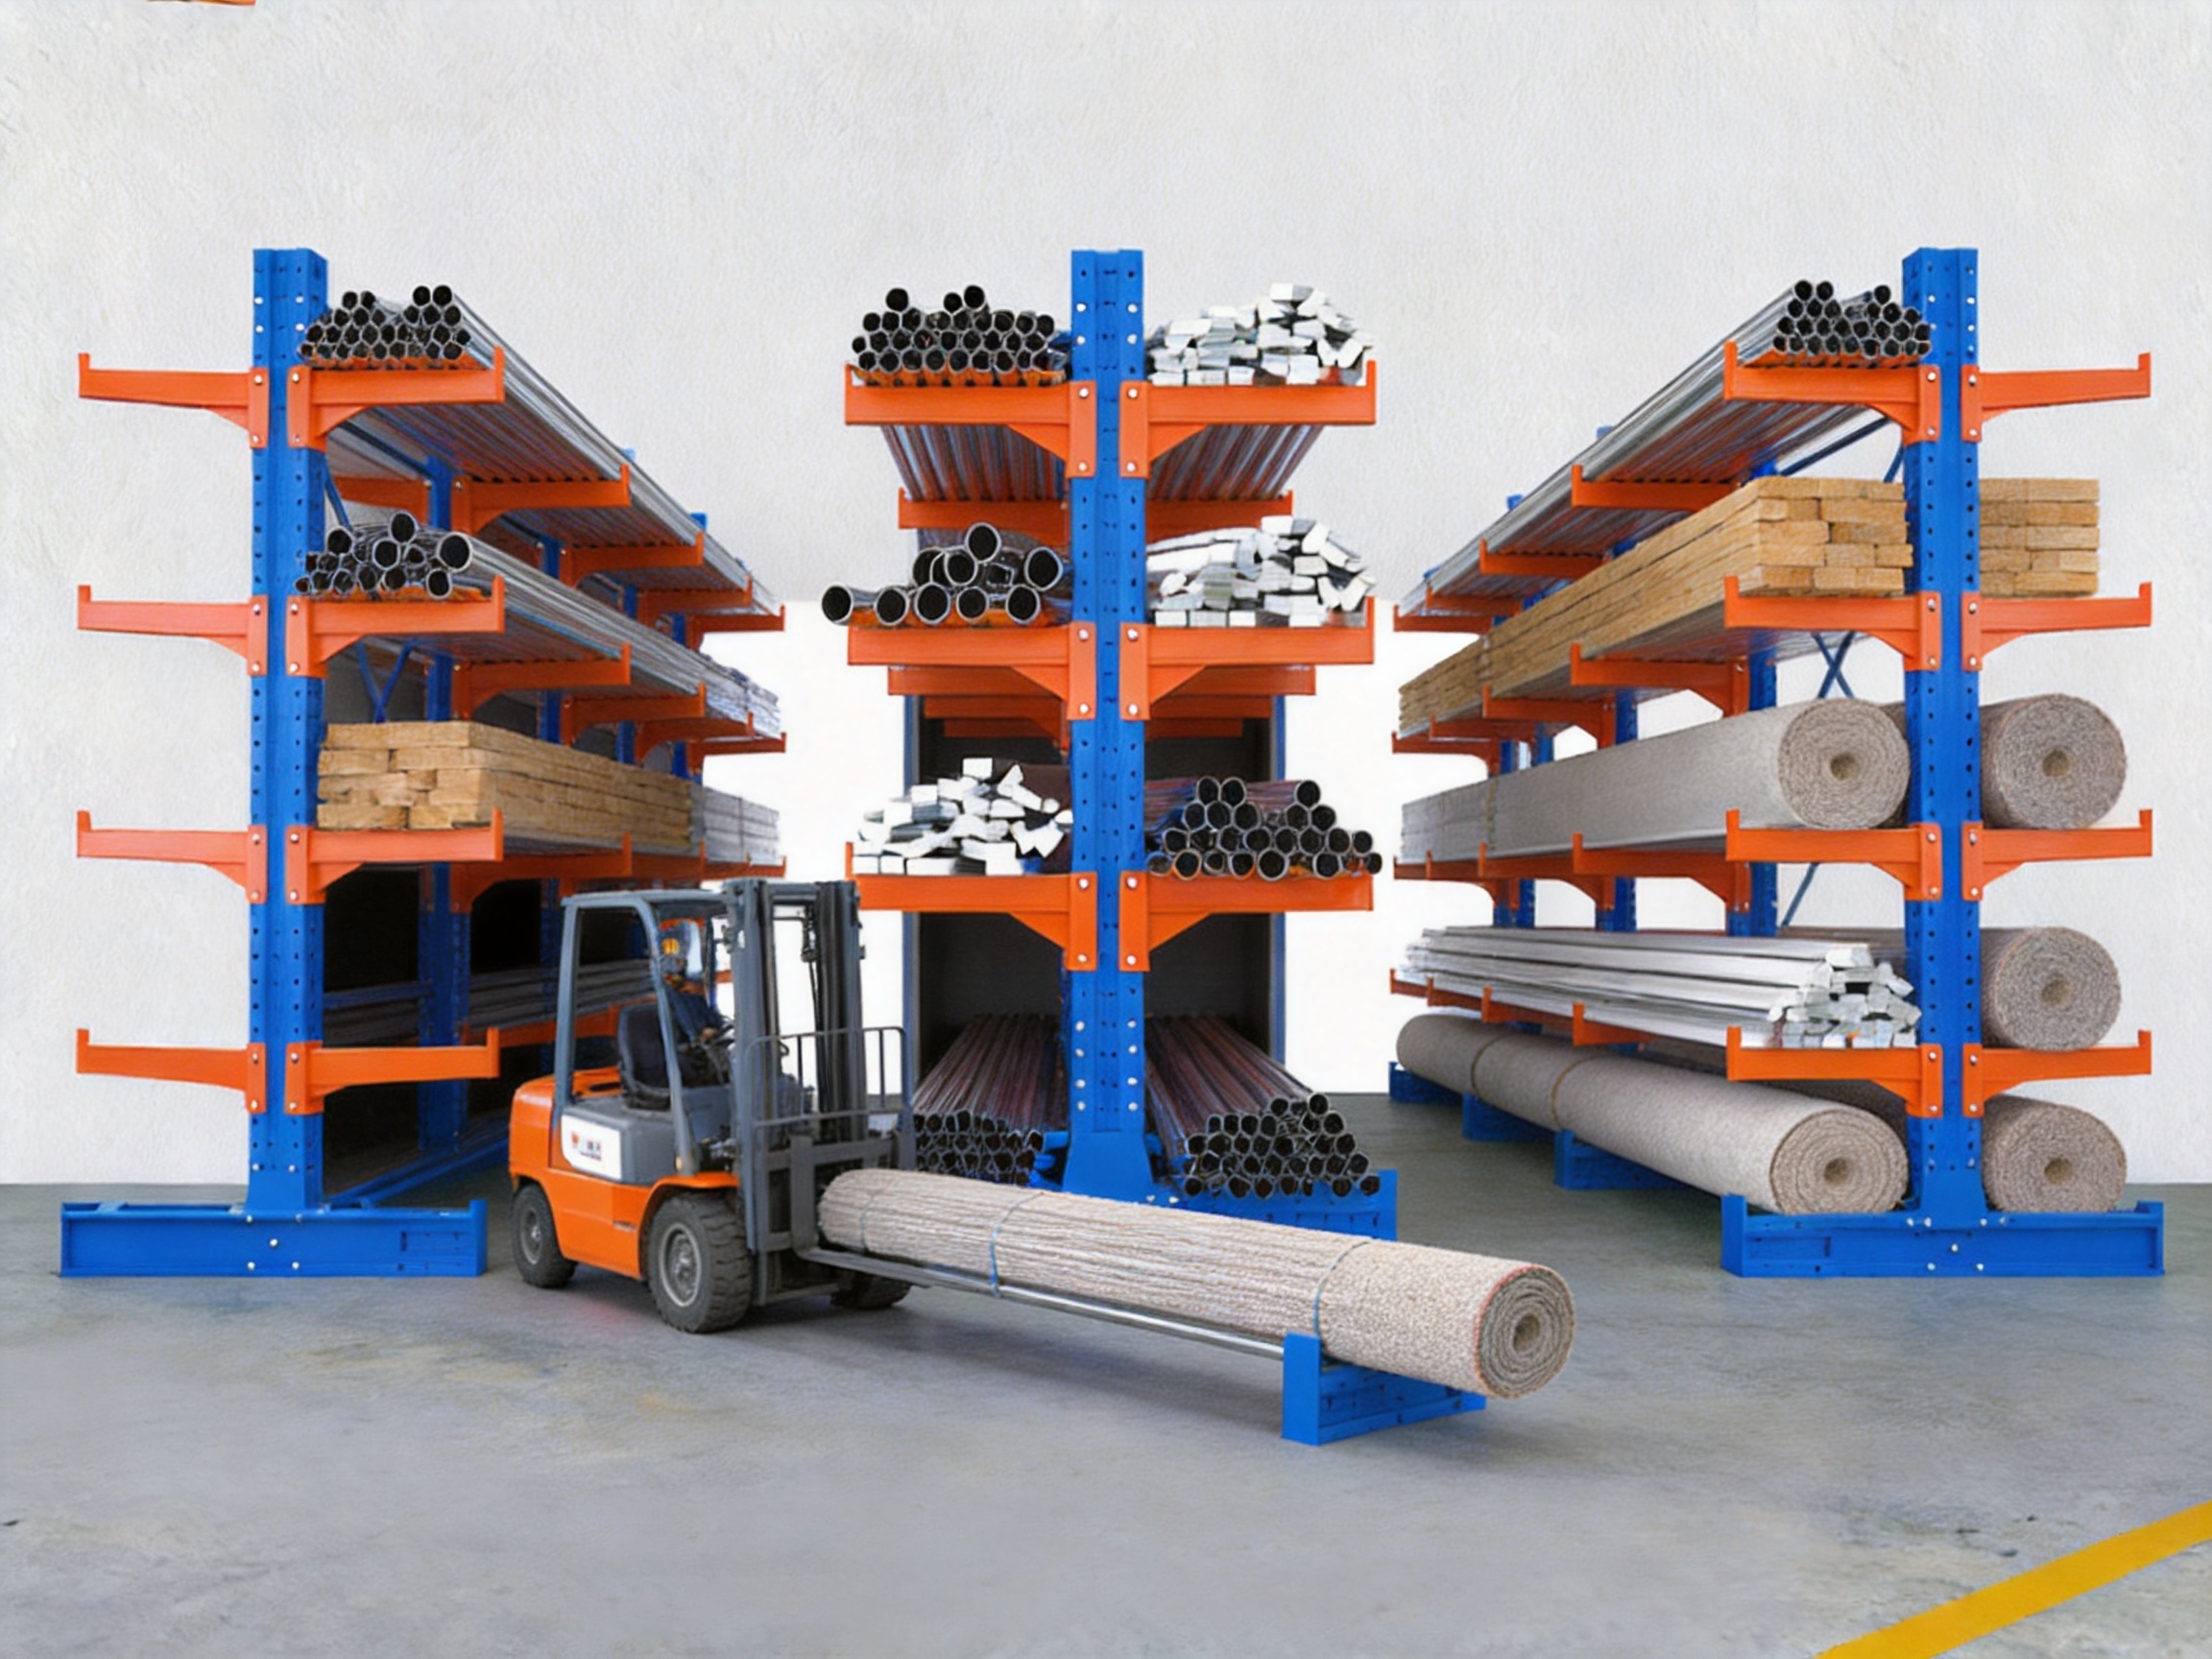
The heavy-duty industrial warehouse storage cantilever shelf rack is designed specifically for these demanding applications. Its open-front structure allows long products to be loaded from the side or front, while reinforced steel columns and horizontal arms create a stable support system for heavy materials. Unlike closed shelving or pallet racking, cantilever racking does not rely on front uprights that obstruct access. This makes it especially suitable for goods that cannot be easily placed into standard rack bays.
Manufactured by Shanghai King Global Shelf Co., Ltd., this cantilever rack reflects the company’s focus on practical storage engineering, customized production, quality control, and international supply capability. The system can be configured for light-duty, medium-duty, or heavy-duty use, with options for different rack lengths, heights, arm capacities, column spacing, and shelf arrangements. It can also be adapted to support changing inventory requirements as a warehouse grows.
This article examines the design, advantages, applications, manufacturing strengths, customization possibilities, and operational value of heavy-duty cantilever storage racks. It also explains how businesses can select the right configuration and use the system safely and efficiently.
Understanding Cantilever Storage Rack Design
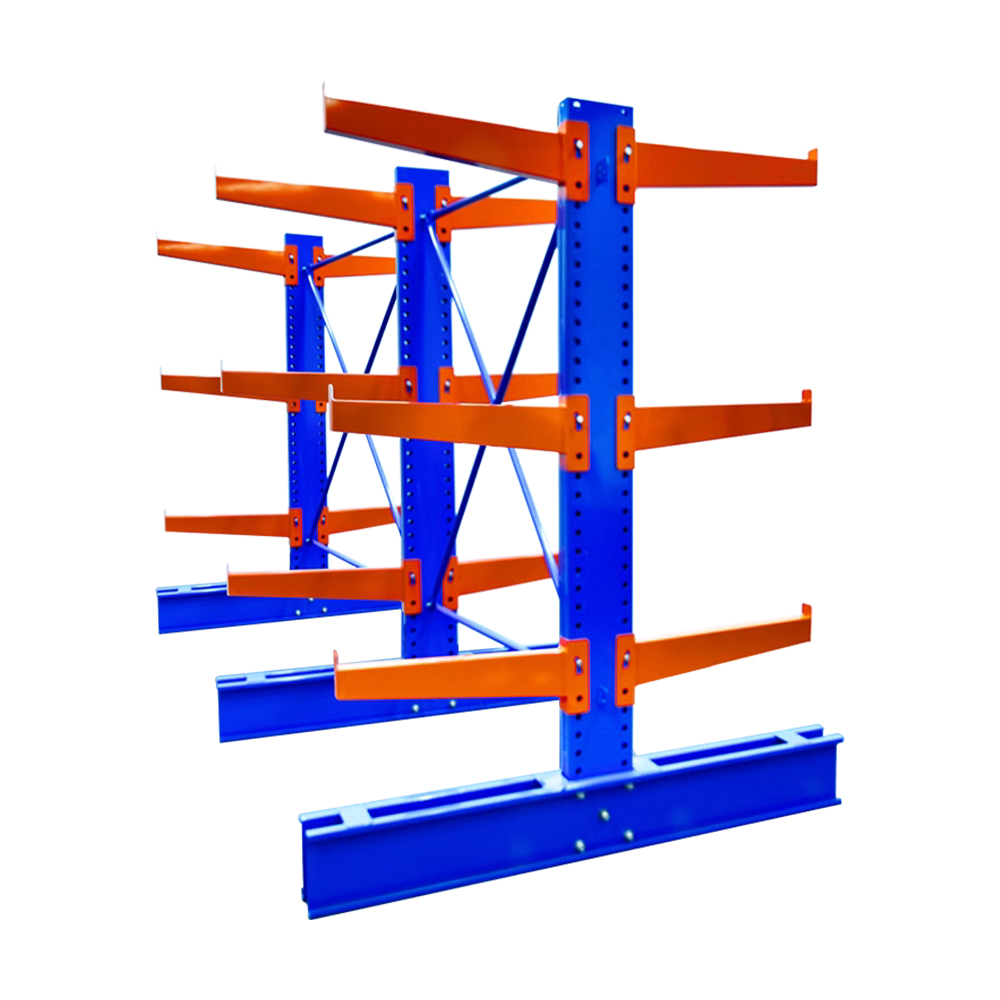
A cantilever rack is a specialized storage structure consisting primarily of vertical columns, horizontal arms, base supports, and stabilizing connections. The arms extend outward from the columns, creating open storage levels without front posts. This configuration provides direct access to long goods and allows forklifts, cranes, pallet jacks, and other handling equipment to approach the load more easily.
The basic structure is simple, but its performance depends on careful engineering. Each vertical column must withstand the combined weight of the arms and stored products. The base must provide sufficient stability against tipping and movement. The arms must support the load evenly while resisting bending. Connections between components must remain secure during repeated loading and unloading.
In a well-designed system, the rack can be installed as a single-sided unit against a wall or as a double-sided unit positioned in the center of a warehouse aisle. Single-sided racks are useful where storage space is located along a wall. Double-sided racks provide access from both directions and maximize the amount of material stored within a given floor area.
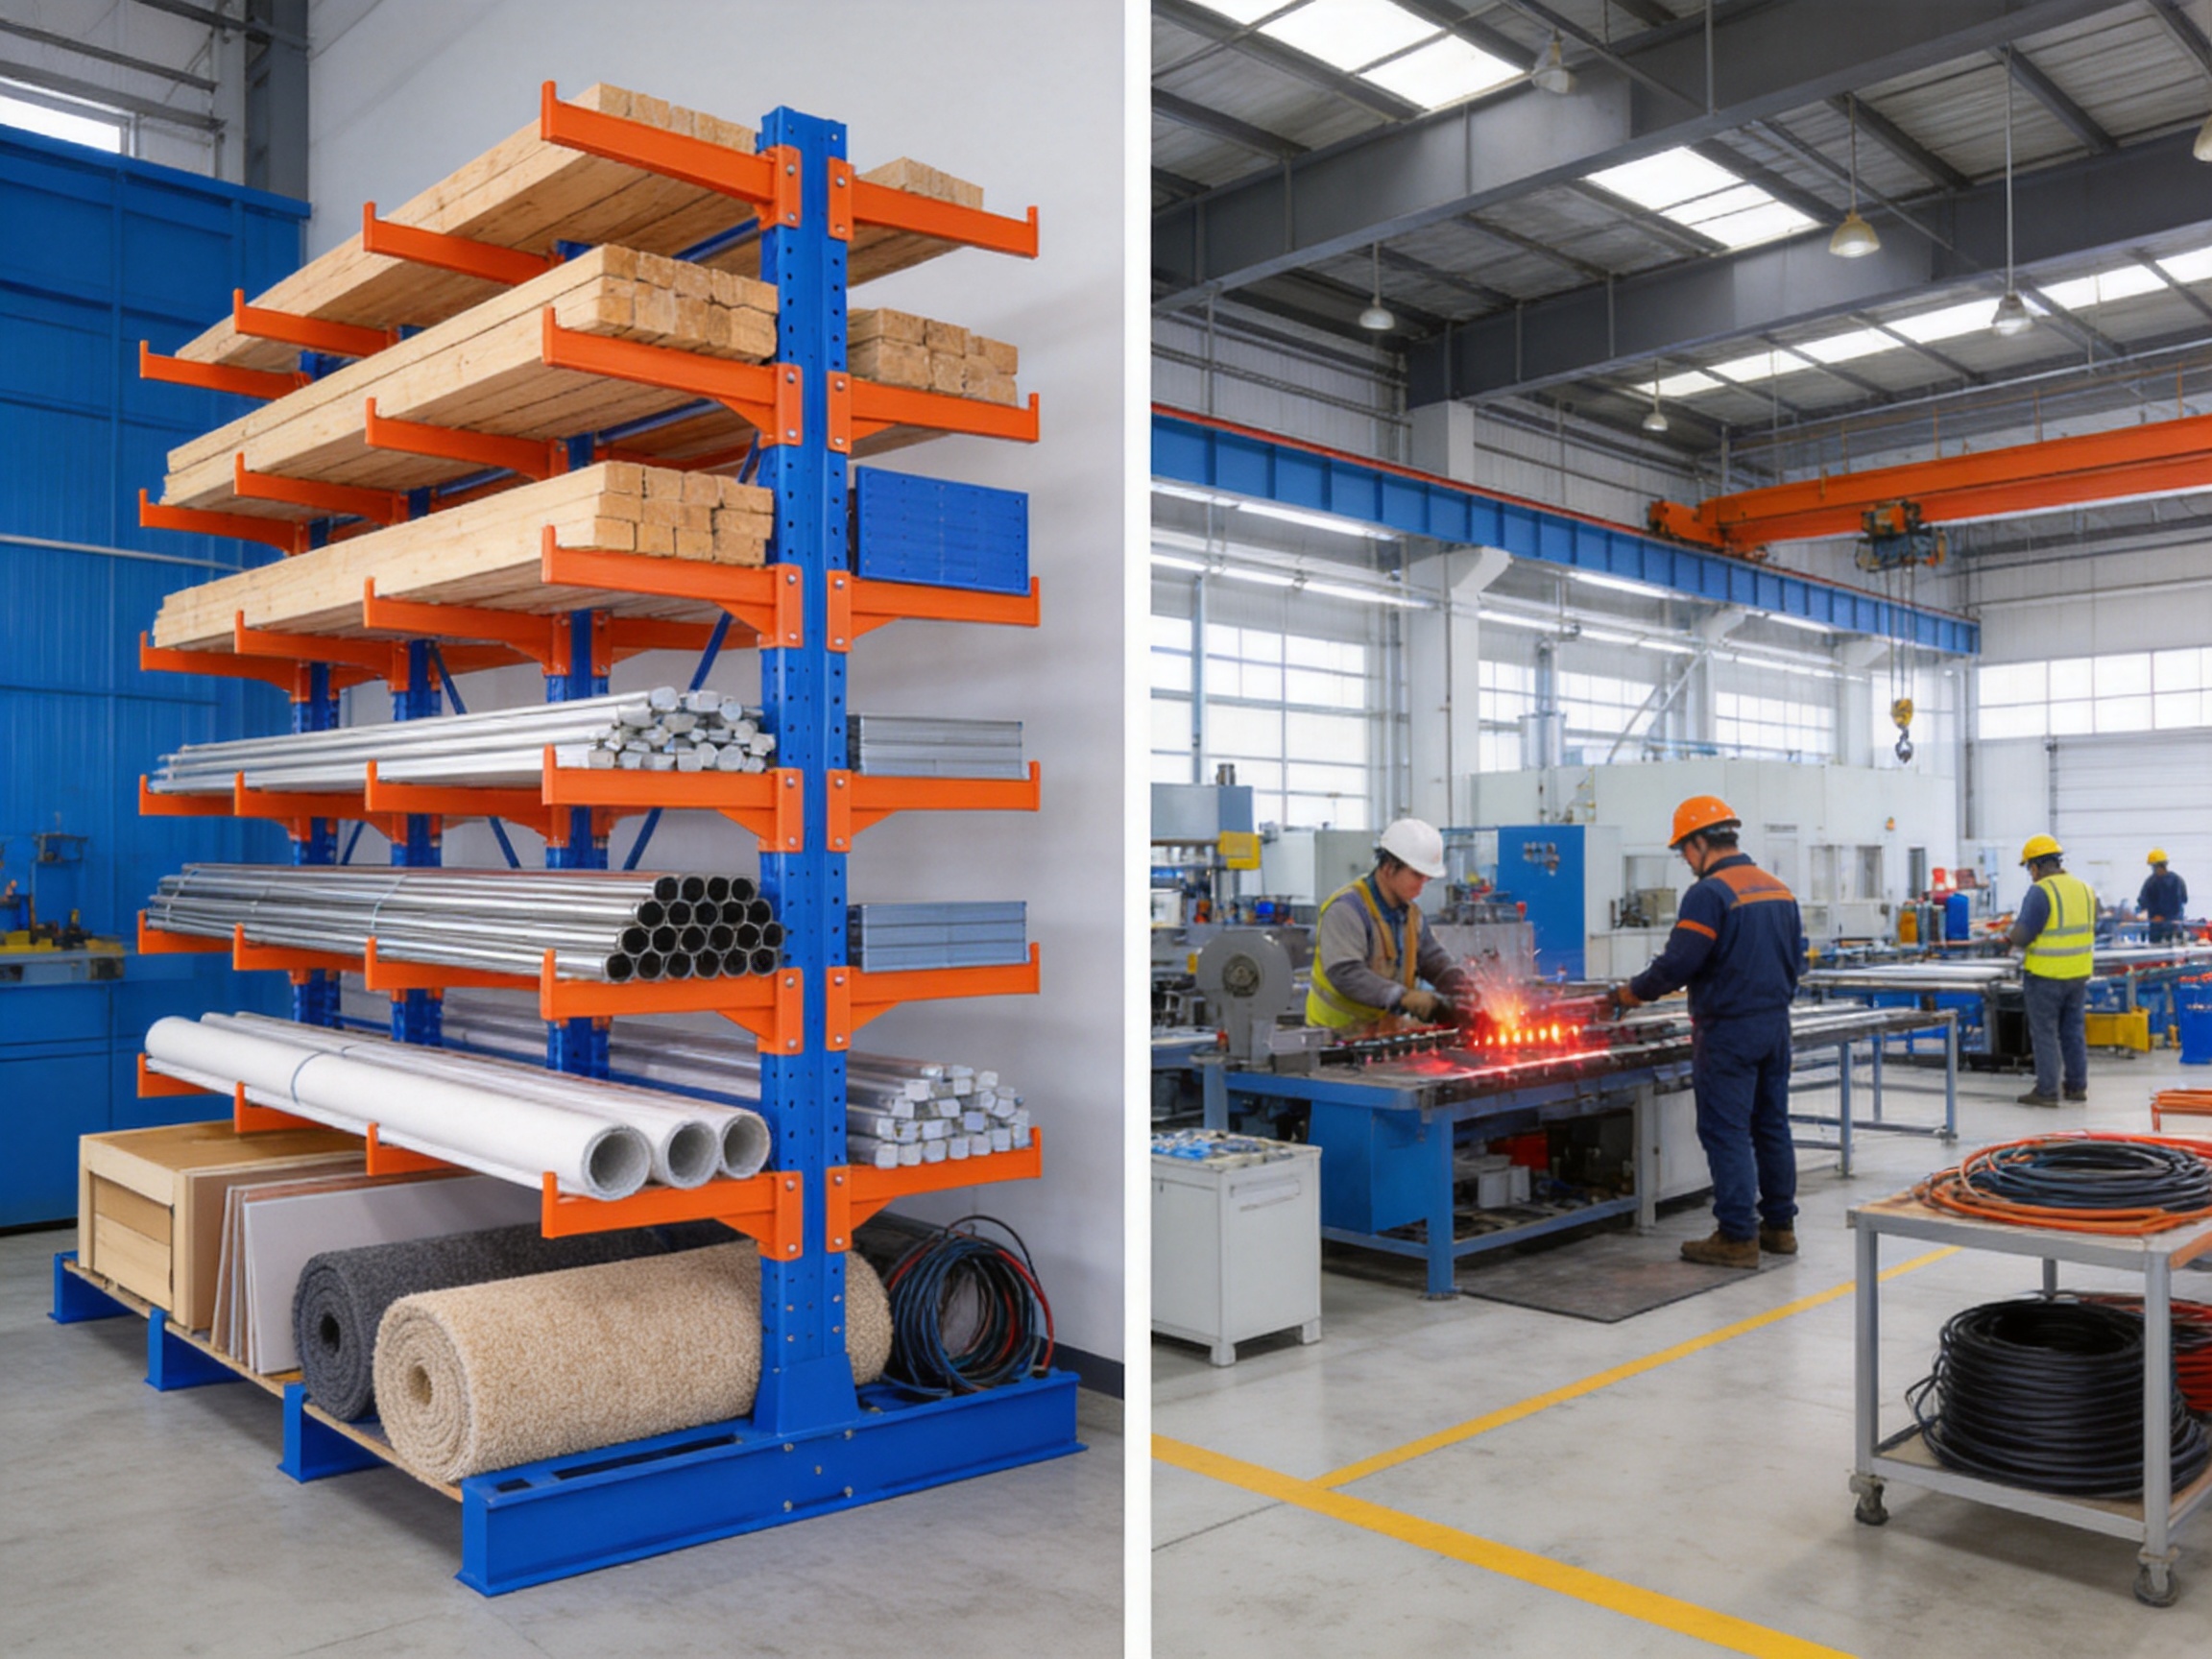
Adjustable arm levels make it possible to store products of different heights. Operators can position the arms according to the dimensions of the goods, avoiding wasted vertical space. Additional shelf panels may be installed when smaller products or low-height items need to be stored alongside long materials.
Key Product Features
Open Access for Long and Oversized Products
The most important advantage of cantilever storage is its unobstructed front. Conventional pallet racks use upright frames at the front and rear of each bay. These frames work well for palletized products, but they can interfere with the storage of long or flexible items. Loading a bundle of pipes or timber into a conventional rack may require additional maneuvering, special pallets, or manual repositioning.
Cantilever racks eliminate much of this difficulty. Products can extend across the arms without being enclosed by front uprights. This makes it easier to position long items with a forklift or crane and reduces the risk of striking rack components during loading. The open design also gives warehouse staff a clearer view of inventory.
Improved visibility supports faster stock identification and order picking. Employees can see product sizes, bundles, and quantities without opening containers or moving multiple pallets. This is particularly valuable in construction material distribution, metal processing, furniture manufacturing, carpet storage, and building supply operations.
Reinforced Steel Construction
The rack is built from heavy-duty steel components selected to withstand demanding industrial conditions. Reinforced columns form the primary vertical support, while horizontal arms distribute the load across the storage levels. The base and structural connections help maintain stability when the rack is loaded, unloaded, or exposed to repeated equipment movement.
Steel construction provides several operational benefits. It resists deformation under properly specified loads, maintains structural integrity over long periods, and supports repeated industrial use. Compared with improvised wooden supports or light commercial shelving, a professionally manufactured steel cantilever system offers more predictable performance and a more organized storage environment.
The actual load capacity of a rack depends on the selected configuration, arm length, column height, spacing, number of levels, load distribution, anchoring method, and installation conditions. For this reason, the correct system should be selected according to the intended application rather than based only on appearance or nominal dimensions.
Flexible Modular Configuration
The modular design allows businesses to specify the rack according to the dimensions and weight of their products. Length, height, width, arm spacing, column spacing, and the number of storage levels can be adjusted to suit a warehouse layout or production process.
Modular construction is especially useful for companies with changing product lines. A warehouse may initially store short timber sections but later begin handling longer metal profiles or larger composite panels. A configurable cantilever system can be designed to accommodate these changes more effectively than fixed-purpose storage furniture.
Adjustable levels also help reduce unused vertical space. Products can be arranged according to height, with closely spaced arms for smaller materials and wider spacing for large bundles. This improves storage density without forcing every item into a standard shelf size.
Optional Shelves for Smaller Goods
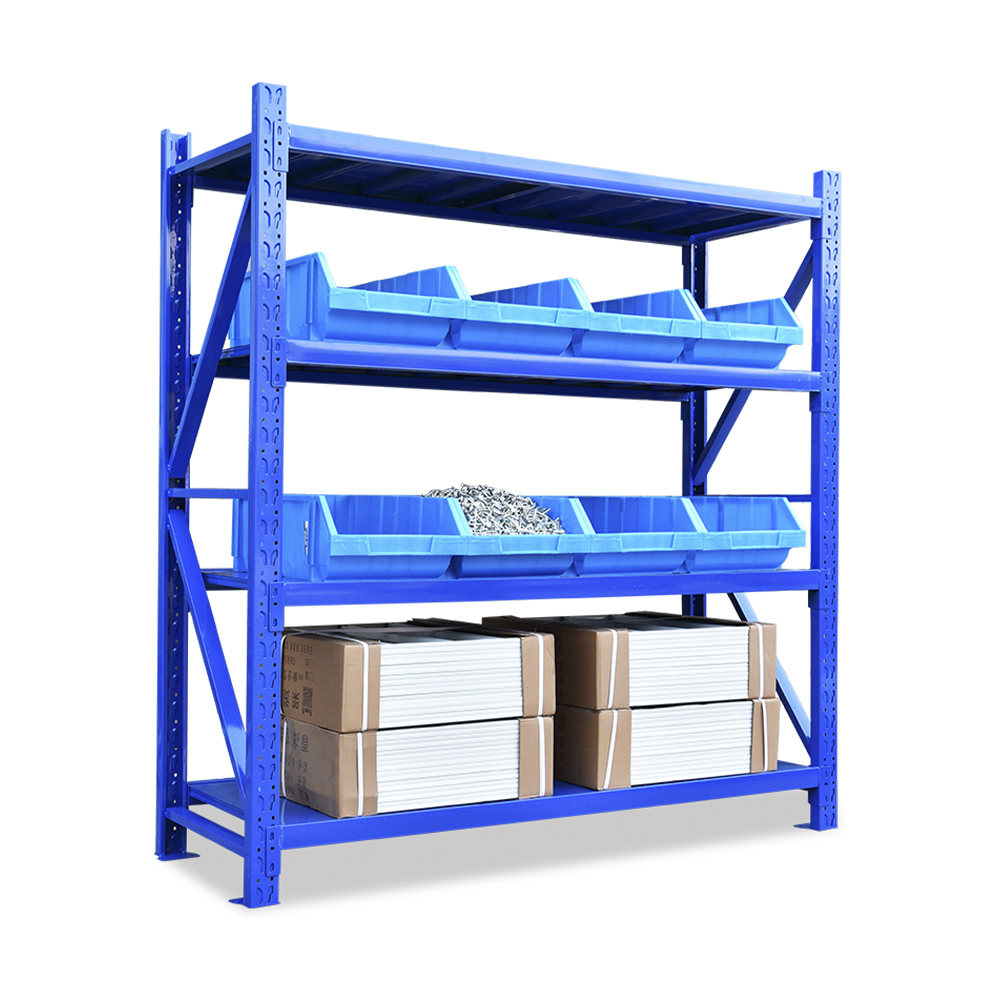
Although cantilever racks are best known for long products, optional shelf panels can increase their versatility. Shelves may be installed on selected levels to hold smaller boxes, fittings, tools, accessories, low-height components, or packaged goods.
This hybrid approach is useful in workshops and distribution centers where long materials and related small parts are handled together. For example, a building materials supplier may store steel channels on the cantilever arms while keeping fasteners, connectors, and protective accessories on shelf panels below or above the main storage levels.
Industrial Powder-Coated Finish
The rack uses a powder coating finish designed to improve resistance to rust, corrosion, scratches, and general wear. Powder coating creates a durable surface layer that is suitable for many warehouse, factory, workshop, and construction environments.
A quality finish contributes more than visual appeal. It helps preserve the steel surface during frequent handling and reduces the effect of minor contact with packaging, equipment, and stored goods. Maintaining the coating through proper cleaning and timely repair of damaged areas can support a longer service life.
Surface treatment requirements may vary according to climate and operating conditions. Indoor facilities with controlled humidity may use a standard industrial coating, while locations with high humidity, corrosive materials, or semi-outdoor exposure may require additional protection. These requirements should be discussed during the design stage.
Heavy-duty Industrial Warehouse Storage Cantilever Shelf Rack
Advantages Compared with Conventional Storage Systems
Compared with Standard Pallet Racking
Pallet racking is highly effective for standardized pallets and boxed inventory, but it is not always appropriate for long, loose, or irregular products. Pallet racks require goods to be placed on pallets or other load carriers. Long products may overhang the pallet, become unstable, or block adjacent positions.
Cantilever racks are designed for direct storage of long goods. The material can rest across several arms, allowing the rack to support the product along its length. This reduces dependence on special pallets and makes the system more suitable for materials that are naturally long or difficult to package.
Cantilever storage can also improve handling efficiency. Operators do not need to place every item inside a pallet cage or maneuver a long product into a confined bay. When the rack is correctly positioned, a forklift can approach the load in a more direct manner.
Compared with Closed Shelving
Closed shelving is suitable for cartons, small parts, documents, and packaged inventory. However, the front and side boundaries of closed shelves can make loading long materials difficult. Products may need to be cut, bent, or placed at an angle, which can create safety and handling problems.
The open structure of a cantilever rack provides a clear loading path. Products can be stored horizontally without being forced into a narrow compartment. This is an important benefit for rigid materials such as steel bars, wood boards, metal tubing, and architectural profiles.
Compared with Floor Stacking
Floor stacking may appear inexpensive, but it often consumes valuable floor area and creates problems with access, product identification, housekeeping, and safety. When long products are stacked directly on the floor, workers may need to move several items before reaching the one required for an order.
Vertical cantilever storage creates organized levels that separate product groups and improve accessibility. It can also reduce the risk of materials being exposed to floor moisture, vehicle traffic, accidental impact, and uncontrolled pile movement.
Better organization can support stock rotation and inventory accuracy. Materials can be assigned to designated rack positions, labeled according to size or grade, and counted more easily during routine checks.
Compared with Improvised Supports
Some facilities use wooden blocks, welded frames, or other improvised structures to hold long goods. While these methods may provide temporary support, they often lack standardized load ratings, consistent dimensions, and long-term durability. They may also be difficult to inspect or modify.
A professionally designed cantilever system provides a more systematic solution. Components are manufactured to repeatable specifications, and the rack can be planned around the expected product weights and handling equipment. This improves consistency across the warehouse and makes future expansion more straightforward.
Applications Across Industrial and Commercial Environments
Lumber and Building Materials
Timber, plywood, molding, flooring, drywall profiles, and other building materials are often long, wide, or difficult to place on standard pallets. Cantilever racks allow these materials to be grouped by length, grade, finish, or application.
Construction supply warehouses can use the system to separate indoor materials from outdoor products, or finished items from raw stock. Rack positions can be labeled so that workers can quickly locate the correct material for customer orders.
Metal and Steel Products
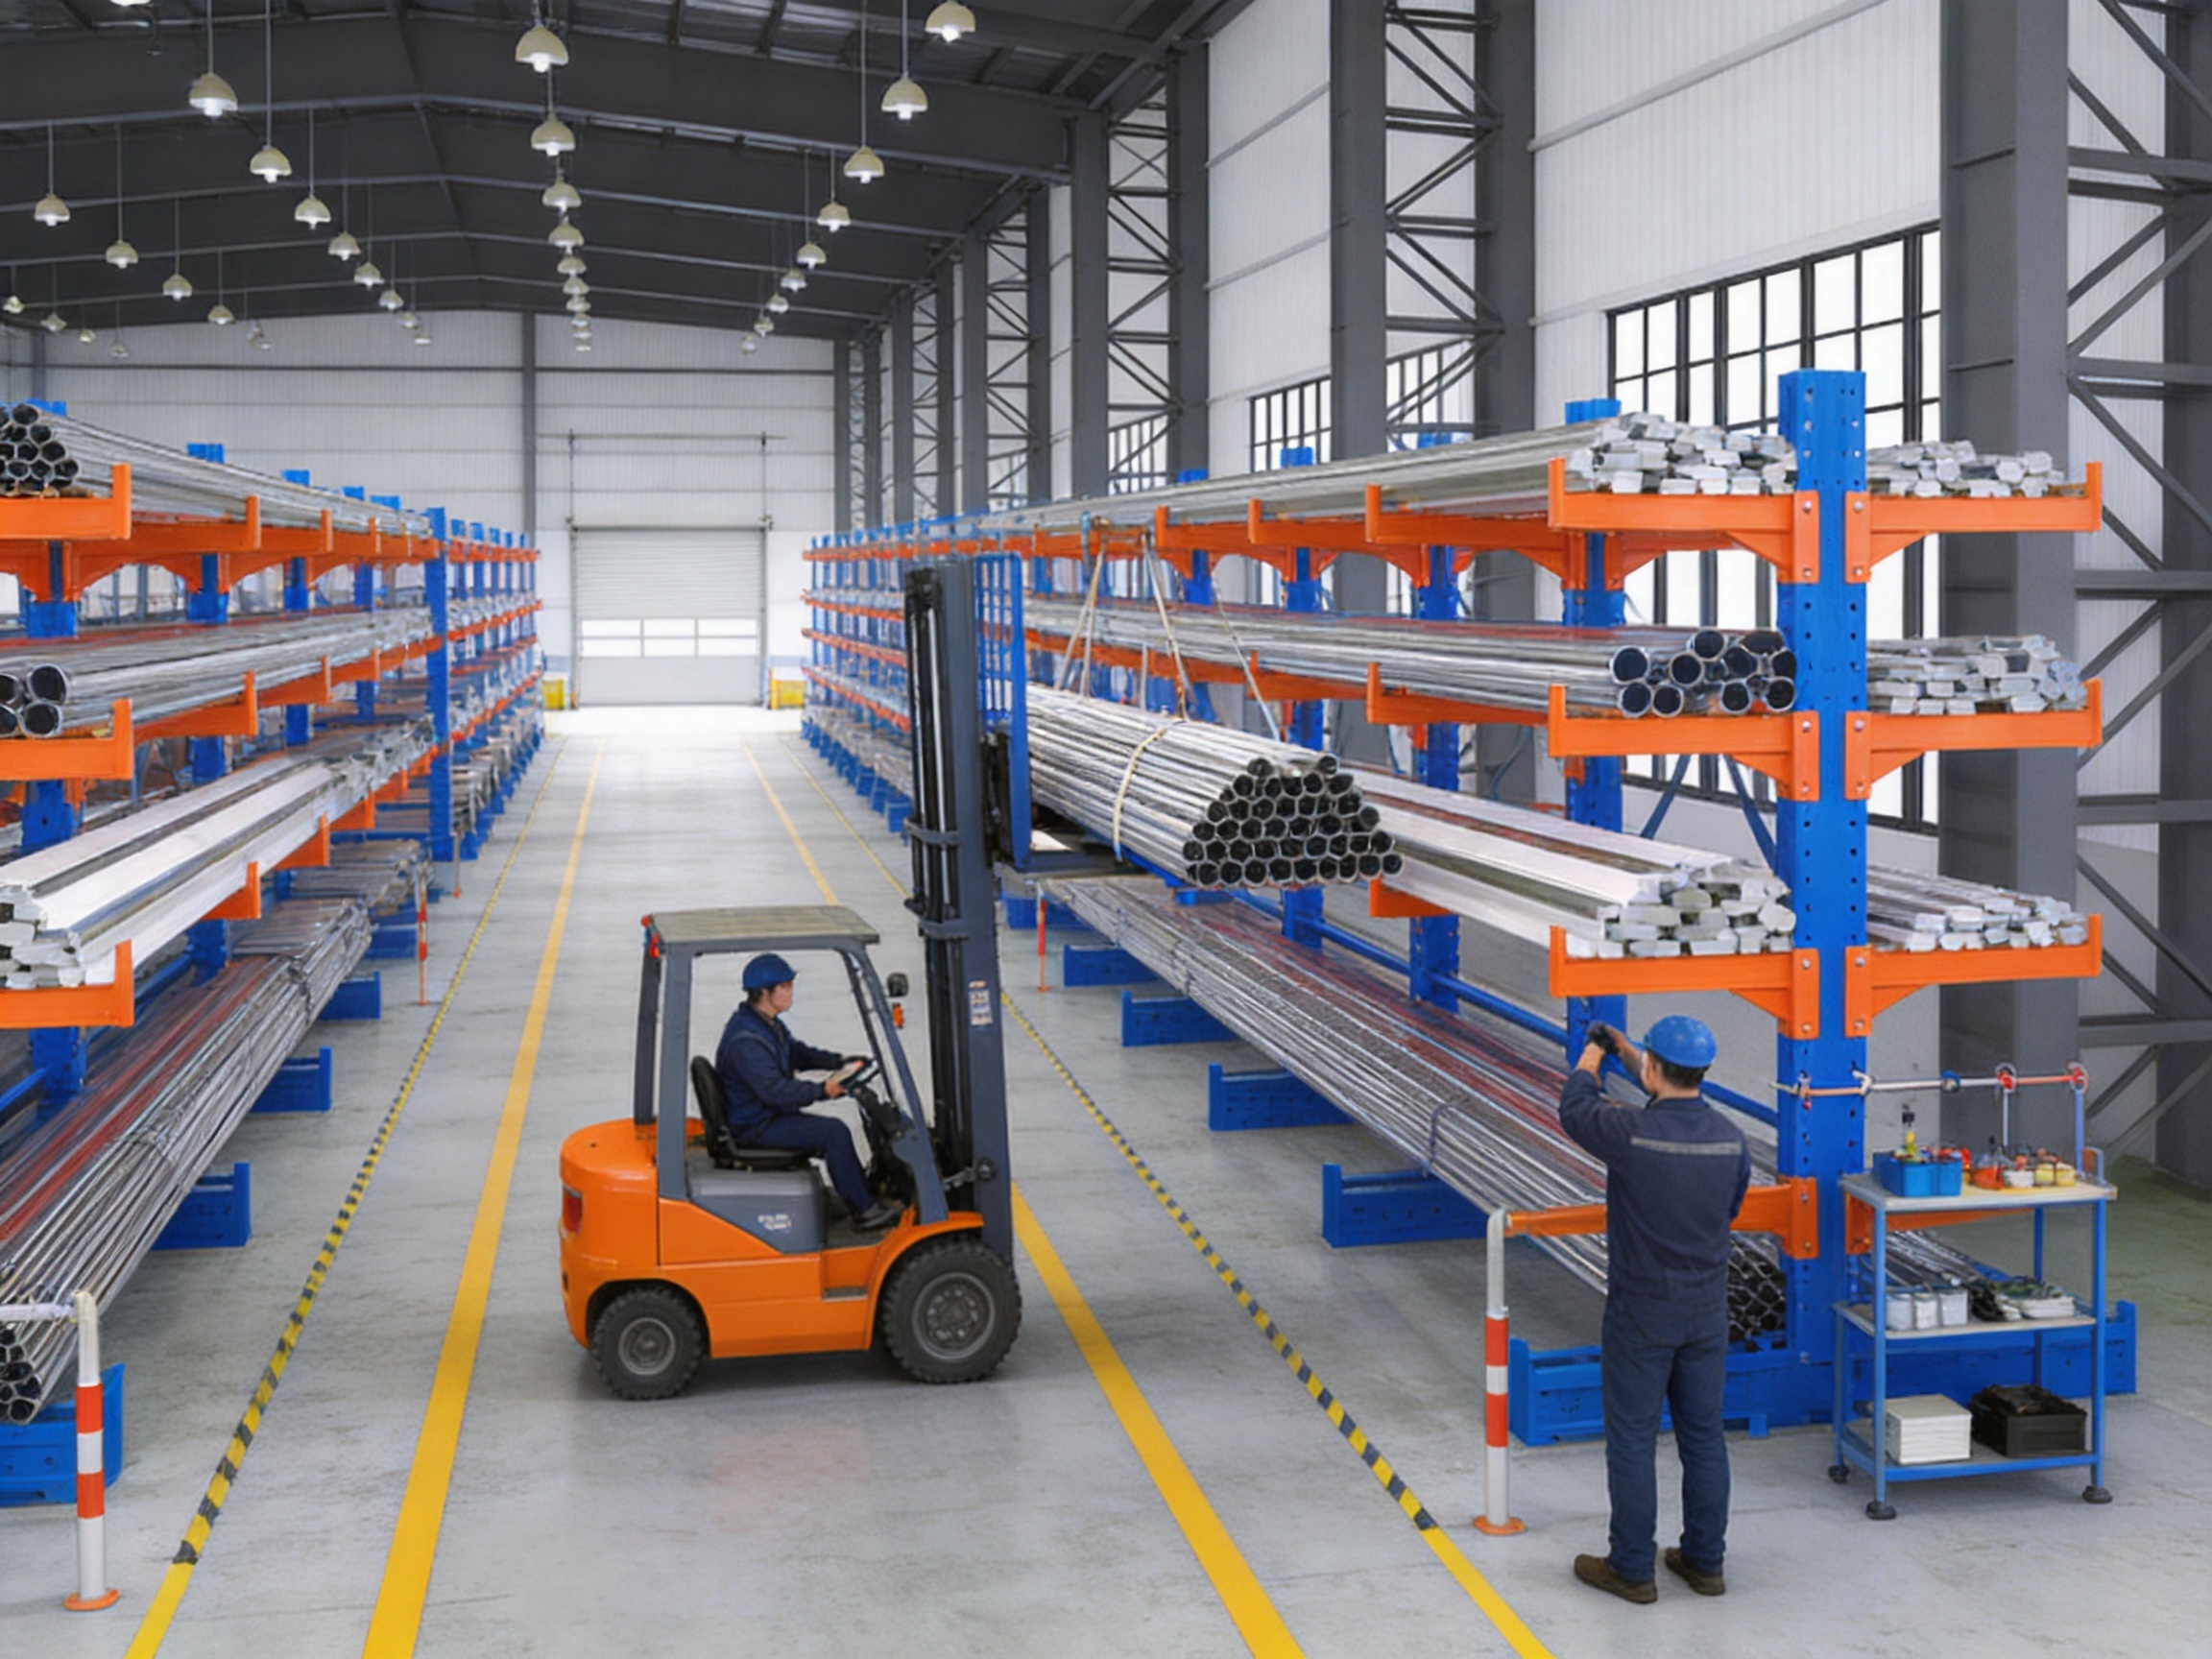
Metal suppliers and fabricators frequently handle steel bars, aluminum profiles, copper tubing, channels, beams, sheets, and pipes. These products may be heavy and may have sharp edges or irregular shapes. A heavy-duty cantilever rack provides a strong support structure while maintaining access for cranes and forklifts.
Different rack levels can be dedicated to different metal grades, dimensions, or processing stages. Materials awaiting cutting can be separated from finished products, reducing confusion and supporting production flow.
Pipe and Tube Storage
Pipe and tube products are often stored in bundles or individual lengths. Their round surfaces can roll when placed on an uncontrolled floor stack. Cantilever arms can be configured with suitable spacing and, where required, additional retaining features or support accessories to help keep products organized.
Proper loading procedures remain essential. Operators should ensure that bundles are centered, evenly distributed, and prevented from rolling or sliding beyond the intended support area.
Carpet, Fabric, and Rolled Materials
Carpet rolls, textile rolls, plastic film, cable, rubber sheets, and other rolled materials can occupy considerable space when stored on the floor. Cantilever systems can be configured for horizontal storage, with arm spacing selected according to roll diameter and weight.
Organized roll storage helps protect the material from unnecessary contact and makes it easier to identify product colors, widths, lengths, and batch information. In some applications, specialized cradles or additional supports may be required to protect the shape of the rolls.
Furniture and Joinery Components
Furniture manufacturers and distributors handle tabletops, doors, panels, frames, trim, and long decorative elements. These products may be too large for ordinary shelving but not suitable for palletized storage. Cantilever racks provide a practical intermediate solution.
Optional shelves can be used for hinges, handles, fittings, hardware, and packaging supplies. Combining long-item storage with small-component shelving can shorten the distance between related inventory categories.
Construction and Maintenance Sites
Construction projects often require temporary storage for reinforcement bars, scaffolding components, pipes, timber, electrical conduit, and other long materials. A modular rack can help organize materials in a site warehouse or distribution yard, provided that the installation environment and anchoring requirements are properly assessed.
Maintenance departments in factories, utilities, and infrastructure facilities can also use cantilever storage for replacement parts, metal stock, cables, and repair materials. Organized storage helps maintenance teams find required components quickly during urgent work.
Manufacturing Strengths and Production Capabilities
The performance of an industrial rack begins with manufacturing discipline. Shanghai King Global Shelf Co., Ltd. specializes in the development, production, and sales of shelving and storage products. Its product scope includes warehouse racks, pallet racking, mezzanine racking, cantilever racks, supermarket shelves, office shelves, and home storage products.
The company was founded in 2010 and has developed an integrated system covering product development, manufacturing, quality control, and market service. This integrated structure allows product requirements to be considered from the early design stage through production, inspection, packaging, delivery, and after-sales support.
Large-Scale Production Base
The company operates a production base covering approximately 60,000 square meters and has more than 300 employees. A production base of this scale can support multiple product categories while providing room for material preparation, forming, welding, coating, assembly, inspection, and finished-goods handling.
For international customers, production capacity is important because projects may involve many rack components, multiple warehouse zones, or repeat orders for expansion. A larger manufacturing organization can help coordinate batch production and maintain consistency between initial and subsequent deliveries.
Product Development and Engineering
Industrial storage systems must be developed around real operating conditions rather than only general dimensions. Product development should consider load distribution, product length, aisle width, forklift access, building height, floor conditions, rack anchoring, and future expansion.
The company’s technical team supports standard products as well as customized OEM and ODM solutions. This is valuable for distributors, contractors, warehouse operators, and equipment integrators that require particular dimensions, finishes, branding arrangements, packaging specifications, or regional market adaptations.
Customization may involve the number of arms, arm length, column height, rack depth, level spacing, base dimensions, color, shelf panels, safety accessories, and connection details. Each change should be assessed against the intended load and operating environment to ensure that the final system remains suitable for its purpose.
Material Preparation and Component Forming
Reliable rack production begins with appropriate steel material and controlled component preparation. Steel sections must be cut accurately so that columns, arms, bases, and braces fit together correctly. Forming operations must maintain consistent dimensions and avoid excessive distortion.
Dimensional accuracy is important for both installation and performance. Components that are inconsistent in length or hole position may create alignment problems during assembly. Accurate preparation helps reduce installation time and supports uniform load transfer through the completed structure.
Welding and Structural Assembly
Welding is commonly used to join structural parts such as base components, reinforcements, brackets, and support members. Consistent welding procedures help ensure that joints provide the intended strength and stability.
After welding, components may require cleaning, inspection, and preparation before coating. Proper treatment helps remove contaminants and supports better coating adhesion. Weld quality, dimensional consistency, and the condition of joints should be checked as part of the production process.
Powder Coating and Surface Protection
Powder coating is an important stage in the manufacturing process. The steel surface is prepared before the powder material is applied and cured. When properly performed, the resulting coating provides a uniform and durable finish that helps protect the rack during industrial use.
Color selection can support warehouse organization. Different colors may be used for different departments, material categories, or customer projects. However, color should complement rather than replace clear labeling and safe operating procedures.
Quality Control
Quality control should be applied throughout the manufacturing cycle rather than only at the end. Material checks, dimensional inspections, weld assessments, coating inspections, assembly verification, and packaging reviews all contribute to product reliability.
For customized projects, quality control is especially important because the product may differ from standard catalog dimensions. Drawings, specifications, approved samples, and inspection records can help ensure that the delivered rack matches the customer’s requirements.
International Market Experience
The company exports products to North America, Southeast Asia, Japan, South Korea, the Middle East, Europe, and other regions. International experience can help a manufacturer understand different warehouse layouts, customer expectations, packaging needs, delivery requirements, and installation practices.
Global supply capability also supports customers who operate in several countries. A consistent manufacturing partner may help maintain similar rack designs and quality expectations across multiple facilities while allowing local adjustments when needed.
Customization Options for Different Storage Requirements
| Configuration Element | Typical Purpose | Important Selection Considerations |
|---|
| Rack height | Uses available vertical space | Building height, sprinkler clearance, lifting equipment, and safe access |
| Rack length | Determines overall storage capacity | Available wall or floor length, product dimensions, and expansion plans |
| Arm length | Supports the depth of stored products | Product width, center of gravity, load distribution, and handling method |
| Arm spacing | Creates suitable storage levels | Product height, bundle size, access requirements, and vertical clearance |
| Single- or double-sided design | Adapts the rack to the warehouse layout | Wall placement, aisle arrangement, and access direction |
| Load capacity | Matches the rack to stored materials | Product weight, quantity per level, arm capacity, and column capacity |
| Optional shelves | Stores small or low-height products | Item size, shelf load, picking method, and required flexibility |
| Surface finish | Provides protection and visual consistency | Humidity, corrosion exposure, indoor or outdoor use, and color requirements |
Light-Duty Configurations
Light-duty cantilever racks are suitable for relatively small or lightweight products such as trim, plastic sections, small tubing, packaging materials, and workshop components. They can provide organized vertical storage without the structural scale required for heavy steel or timber bundles.
Even light-duty systems must be loaded within their specified capacity. Long products may create leverage forces that are different from those produced by compact boxes, so product length and distribution should be considered during selection.
Medium-Duty Configurations
Medium-duty racks can support a broad range of commercial and industrial materials. They may be used by building supply distributors, furniture factories, maintenance departments, and general warehouses handling mixed long products.
This category often provides a balance between capacity, flexibility, and investment. Adjustable levels and optional shelves can make the system suitable for facilities that store several product types rather than one standardized material.
Heavy-Duty Configurations
Heavy-duty cantilever racks are intended for demanding applications involving substantial loads such as steel bars, large timber bundles, heavy pipes, structural profiles, and industrial rolls. These systems require careful engineering and accurate load information.
Heavy-duty performance depends on the complete rack configuration, not only the thickness of one component. Columns, arms, bases, braces, anchors, and floor conditions must work together. Professional design support is recommended when products are particularly heavy, long, dense, or difficult to control.
Warehouse Layout and Space Utilization
A cantilever rack should be positioned as part of an overall warehouse layout rather than treated as an isolated piece of equipment. The design should consider receiving areas, inspection zones, production lines, dispatch areas, pedestrian paths, emergency routes, and equipment turning space.
Rack height should be coordinated with the building’s clear height and any overhead services. Adequate clearance must be maintained around lighting, sprinklers, ventilation equipment, beams, doors, and other building features. The rack should not obstruct emergency equipment or reduce required access routes.
Aisle width must be compatible with the turning radius and operating method of the forklift or other handling equipment. If long loads require additional maneuvering room, the aisle should not be designed only around the empty vehicle. The length, width, and stability of the load must be included in the layout assessment.
Products should be grouped according to handling frequency, weight, length, and order sequence. Frequently accessed materials can be placed in convenient positions, while slower-moving stock may be assigned to less central areas. Heavier products are generally best positioned at lower levels to reduce handling risks and improve overall stability.
Clear labels and location codes can further improve warehouse efficiency. A simple system may identify the rack row, column, level, and product category. Digital inventory systems can use the same location structure to help workers find and count materials.
Safe Loading and Daily Operation
Load Distribution
Materials should be distributed evenly across the appropriate arms. Concentrating excessive weight at one end or placing a load beyond the intended support area can create unbalanced forces. Bundles should be centered whenever possible, and the weight of each storage level should remain within its specified rating.
Long products should be supported at enough points to prevent excessive sagging. Flexible products may require additional supports or a different arrangement from rigid materials. The storage plan should reflect the physical behavior of the goods, not only their total weight.
Forklift and Crane Access
The open design supports access by forklifts, pallet jacks, cranes, and other wide-load handling equipment. Operators must still approach slowly, maintain visibility, and avoid contact with columns, arms, and adjacent stored products.
Forklift drivers should be trained to account for load length. A long bundle may swing during turning or extend beyond the vehicle. The operator should verify that the path is clear and should not lift or move loads that are unstable, damaged, or improperly bundled.
Inspection and Maintenance
Regular inspections help identify damage before it becomes a serious problem. Warehouse managers should check columns, arms, bases, braces, connectors, anchors, and protective coatings. Bent components, cracked welds, loose connections, missing safety parts, and significant corrosion should be reported and assessed promptly.
Damaged rack components should not be straightened or repaired informally unless the repair has been evaluated by a qualified professional. Removing a damaged arm or unloading the affected bay may be necessary until corrective work is completed.
The surrounding floor should also be kept clean and free from obstacles. Oil, water, packaging debris, and loose materials can increase the risk of slips, collisions, or unstable loading. Good housekeeping supports both rack safety and general warehouse efficiency.
Operator Training
Employees should understand the rack’s intended capacity, loading direction, prohibited practices, and inspection procedures. Training should include safe forklift operation, product bundling, use of protective equipment, communication between workers, and emergency response.
Visual signs can reinforce important rules, but signs are most effective when supported by regular supervision and practical instruction. New employees should receive orientation before handling materials, and refresher training should be provided when layouts, equipment, or products change.
Installation Considerations
Installation quality directly affects rack performance. The floor must be evaluated for levelness, strength, and suitability for anchors. A rack that is correctly manufactured but installed on an unsuitable surface may not provide the expected stability.
Components should be assembled according to approved drawings and instructions. Columns must be aligned, bases must be properly secured, and arms must be installed at the correct levels. All bolts, connectors, braces, and retaining elements should be checked before the rack is loaded.
The installation area should be cleared of unnecessary equipment and materials. A safe assembly sequence reduces the chance of accidental contact or falling components. Depending on rack size and site conditions, professional installation may be appropriate.
After installation, the system should be reviewed before use. The review should confirm dimensions, access clearances, anchoring, level alignment, signage, load information, and compatibility with handling equipment. Any changes requested after installation should be evaluated rather than made casually.
Why Choose a Professional OEM and ODM Manufacturer
Purchasing from a professional manufacturer provides advantages beyond the physical rack itself. A manufacturer with product development, production, quality control, and service capabilities can help customers move from a general storage problem to a practical engineered solution.
OEM capability is useful for distributors and project suppliers that need products manufactured to their own specifications or market requirements. ODM capability is valuable for customers seeking design assistance, modified structures, private-label products, packaging adaptations, or complete storage concepts.
Shanghai King Global Shelf Co., Ltd. offers both standard products and customized solutions for warehouses, supermarkets, offices, homes, and industrial environments. Its broad product range allows customers to coordinate different storage categories through one supplier. A project may combine cantilever racks for long materials, pallet racking for boxed goods, mezzanine systems for additional floor space, and supermarket shelving for retail display.
Supplier continuity can also simplify future expansion. If a business opens another facility or increases its storage capacity, working with an established manufacturer may make it easier to match the original dimensions, finish, and component style.
Manufacturing scale, technical experience, export knowledge, and service coordination are especially important for large projects. Customers may require drawings, quotations, production schedules, packaging plans, shipping coordination, installation support, and replacement components. A structured supplier can help manage these requirements more effectively than an informal fabricator.
Environmental and Operational Benefits
Although the primary purpose of a cantilever rack is storage, better organization can contribute to more efficient facility operation. Vertical use of space may reduce the need for additional floor area, while improved product access can shorten travel and handling time.
When materials are easier to identify and retrieve, businesses may reduce unnecessary movement, duplicate purchases, and product damage caused by repeated restacking. A more organized warehouse can also support better stock rotation and reduce time spent searching for items.
Steel storage systems can remain in service for many years when properly designed, installed, loaded, and maintained. Long service life may reduce the frequency of replacement and the amount of material required for repeated storage equipment purchases.
At the end of its useful life, steel is widely recyclable. Businesses should follow local recycling and disposal requirements and should separate reusable components from damaged materials where practical.
Purchasing Checklist
Before ordering a cantilever storage system, customers should prepare accurate information about the intended application. The following questions can help establish an appropriate specification.
First, identify the products to be stored. Record their length, width, height, weight, shape, packaging method, flexibility, and tendency to roll or shift. If several products will share the rack, include the full range of dimensions and weights.
Second, determine the required storage quantity. Estimate the number of bundles, individual pieces, rolls, or product groups that must be stored at one time. Include expected growth rather than designing only for current inventory.
Third, review the facility. Measure the available length, width, and height, and note doors, columns, walls, sprinkler systems, overhead structures, pedestrian routes, and vehicle paths.
Fourth, identify the handling equipment. The type of forklift, crane, pallet jack, or manual handling method will influence aisle width, rack height, load approach, and storage level spacing.
Fifth, discuss the operating environment. Humidity, temperature, outdoor exposure, chemical contact, dust, and cleaning methods may affect the required surface finish and protection level.
Finally, confirm the documentation and service requirements. Customers may need layout drawings, load information, assembly instructions, inspection guidance, spare parts, installation support, or repeat-order coordination.
Q&A: Common Questions About Cantilever Racks
What products are best suited to cantilever racks?
Cantilever racks are best suited to long, bulky, irregularly shaped, or oversized products. Common examples include pipes, timber, steel bars, metal profiles, carpet rolls, cables, furniture panels, plastic sections, and construction materials.
Can a cantilever rack store short products?
Yes. Short products can be stored if their dimensions and weight are compatible with the rack. Optional shelf panels can make the system more suitable for small boxes, low-height parts, tools, and accessories.
Are cantilever racks available in different load capacities?
Yes. The system can be configured for light-duty, medium-duty, or heavy-duty applications. Capacity must be determined according to the complete design, including the columns, arms, bases, spacing, anchoring, and load distribution.
Can the rack be used on one side only?
Yes. Single-sided racks can be installed against a wall or along the edge of a storage area. Double-sided racks can be positioned in open warehouse space and accessed from both sides.
Can the dimensions be customized?
Yes. Rack height, length, depth, arm length, level spacing, column spacing, shelf options, finish, and other features may be customized according to the project requirements. Custom dimensions should be reviewed by the manufacturer’s technical team.
Can forklifts load and unload the rack?
Yes. The open design is intended to support access by forklifts and other wide-load handling equipment. Operators must use suitable equipment, maintain clear visibility, approach carefully, and follow the specified loading procedures.
What finish is used on the rack?
The rack uses an industrial powder coating finish designed to improve resistance to rust, corrosion, scratches, and daily wear. The most suitable finish may depend on the facility’s humidity, chemical exposure, and indoor or outdoor conditions.
How should the rack be maintained?
Regularly inspect columns, arms, bases, braces, connections, anchors, and coating condition. Keep the surrounding area clean, remove damaged components from service, and arrange professional assessment when structural damage is found.
Can the rack be expanded later?
Many modular configurations can be expanded or modified, subject to available space, structural compatibility, and the requirements of the original design. Expansion should be planned with the manufacturer or a qualified storage-system professional.
Why is professional design important for heavy loads?
Heavy or long products create forces that depend on weight, length, position, and distribution. Professional design helps ensure that columns, arms, bases, anchors, aisles, and handling methods are considered together rather than selected separately.
What industries commonly use cantilever racks?
Common users include lumber suppliers, steel distributors, pipe manufacturers, furniture factories, construction companies, carpet warehouses, maintenance departments, logistics providers, and general industrial storage facilities.
Can one supplier provide other storage products?
Yes. Shanghai King Global Shelf Co., Ltd. manufactures and supplies multiple storage categories, including pallet racking, warehouse shelving, mezzanine racking, supermarket shelves, office shelves, home shelves, and cantilever racks. This can help customers coordinate complete storage projects.
Conclusion
The heavy-duty industrial warehouse storage cantilever shelf rack is a practical solution for businesses that handle long, heavy, irregular, or oversized materials. Its open-front design improves accessibility, its reinforced steel structure supports demanding loads, and its modular format allows the system to be adapted to different warehouse layouts and product categories.
Compared with conventional pallet racking, closed shelving, floor stacking, and improvised supports, cantilever storage can provide better access, more effective vertical organization, and improved compatibility with long-load handling equipment. Optional shelves further extend its usefulness by allowing smaller products and related accessories to be stored within the same organized area.
The value of the product also depends on the strength of its manufacturing partner. Shanghai King Global Shelf Co., Ltd. combines product development, large-scale manufacturing, quality control, customization, and international market experience. Its production base, technical team, broad storage-product range, and OEM/ODM capabilities support customers seeking both standard rack systems and engineered storage solutions.
For the best result, customers should provide accurate product information, facility measurements, handling-equipment details, environmental conditions, and future expansion plans. With appropriate design, installation, loading, inspection, and maintenance, a cantilever rack can improve space utilization, warehouse productivity, inventory visibility, and long-term storage safety.
References
1. General principles of industrial storage-rack design, load distribution, and warehouse planning.
2. Guidance on safe forklift operation, long-load handling, and warehouse traffic management.
3. Best practices for steel fabrication, welding inspection, structural assembly, and industrial powder coating.
4. Warehouse housekeeping and routine inspection principles for industrial storage equipment.
5. Manufacturer-provided product information for heavy-duty industrial cantilever storage rack systems.
6. Manufacturer information concerning customized OEM and ODM shelving and storage solutions.


 English
 Español
 русский
 Français
 한국어
 عربى
 ไทย
 Deutsch
 Bahasa Melayu
 Português
 Polskie